


Introduction — Scenario, Data, Question
I’ll be blunt: shops still lose hours every week to machines that should run unattended. CNC equipment manufacturers know this pain — I’m talking missed cycles, unexpected spindle failures, and the cost that sneaks up on you when uptime dips below target. (In my experience, a mid-sized factory reporting 95% uptime still hides thousands of dollars in avoidable downtime.)
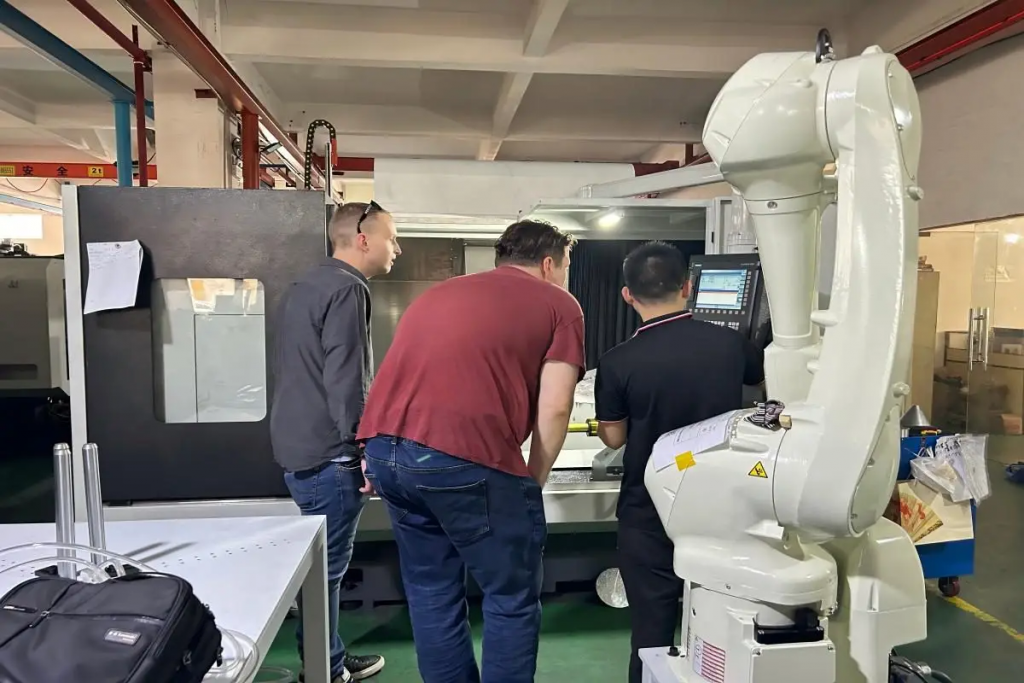
Data backs it up: recent supply-chain and OEE studies show small-to-mid shops average 88–92% utilization across mixed fleets, not because the hardware is weak, but because integration and diagnostics lag. So, what do we fix first — the controller firmware, the toolpath strategy, or the visibility layer that never quite tells the full story?
I want to walk you through what I’ve seen work and what keeps tripping teams up — candid, jargon-forward, but practical. We’ll talk edge computing nodes, servo motors, and real shop-floor tradeoffs. — Let’s move into the nuts and bolts.
Part 1 — Where Traditional Solutions Break Down (Technical Rhythm)
What’s the catch?
I’ve spent time on the floor and behind the dashboards; here’s the blunt assessment: most sellers still pitch the machine as the whole solution. But when buyers search for a reliable option they type cnc machine for sale and expect performance out of the box. That expectation collides with reality. The CNC controller may be solid, but the integration with PLCs, the quality of linear guideways, and the lack of predictive analytics leave gaps. Toolpath optimization is frequently outsourced to CAM defaults — which is fine until a complex pocketing job throws a thermal drift problem. Then the spindle trips. Then you lose a shift.
Technically speaking, legacy fixes focus on stronger power converters or stiffer beds — and yes, those matter — but they’re surface-level. The deeper issues are often in signal fidelity, poorly tuned servo motors, and inconsistent tooling data (tool offsets, wear compensation). We’ve seen inexpensive diagnostic overlays reduce mean time to repair (MTTR) by 20% simply by surfacing tool-life trends. Look, it’s simpler than you think: better telemetry and standardized event logs beat guesswork every time. I’m not saying bolts and castings don’t matter — they do — but the real ROI often lives in data fidelity and automated fault isolation.
Part 2 — Future Outlook: Case Example and Comparative Perspective
Real-world Impact — What’s Next?
I worked with a fabricator who retrofitted three cells with lightweight edge computing nodes and a small-scale MES bridge — they kept the legacy CNC controllers but added an intermediate layer for real-time tool and axis monitoring. The immediate result was fewer nuisance stops; the downstream benefit was better scheduled maintenance windows and fewer rush orders. — funny how that works, right?
Comparatively, another shop invested only in heavier-duty machinery and ignored data integration. Short-term pride, long-term headaches. My takeaway: pairing hardware upgrades with software-driven visibility (simple dashboards, event-driven alerts, basic SPC loops) yields measurable throughput gains faster than hardware-first strategies. If you’re evaluating a cnc automation machine — yes, consider rigidity and torque curves — but don’t skip the telemetry layer that tells you why a part failed before it ruins a batch.
Closing — Three Practical Evaluation Metrics
Here’s what I recommend when you’re sizing options and comparing vendors: first, measure diagnostic granularity — can the system report axis vibration, spindle current spikes, and tool-life per cycle? Second, assess integration friction — does the controller speak modern protocols (MTConnect/OPC UA) or will you need custom translators? Third, quantify maintainability — spare parts lead times, remote-update capability, and how the vendor supports firmware/parameter tuning. These three metrics map directly to lower MTTR and higher effective uptime.
Weigh these against capital cost, but don’t let sticker price blind you. In my view, the machines that last are those designed for observability as much as for metal cutting. — and yes, I’ve changed my mind on that over the years. For real-world sourcing and to see models that balance both hardware and software layers, check out Leichman. I’ll keep testing and sharing what works — because I’d rather save you the hard lessons I learned the long way.
